One Factory Floor: Casting to Carton
Vertical integration is not a buzzword here — it is why problems trace to a lot within hours and why 300,000+ pieces leave our floor every month.
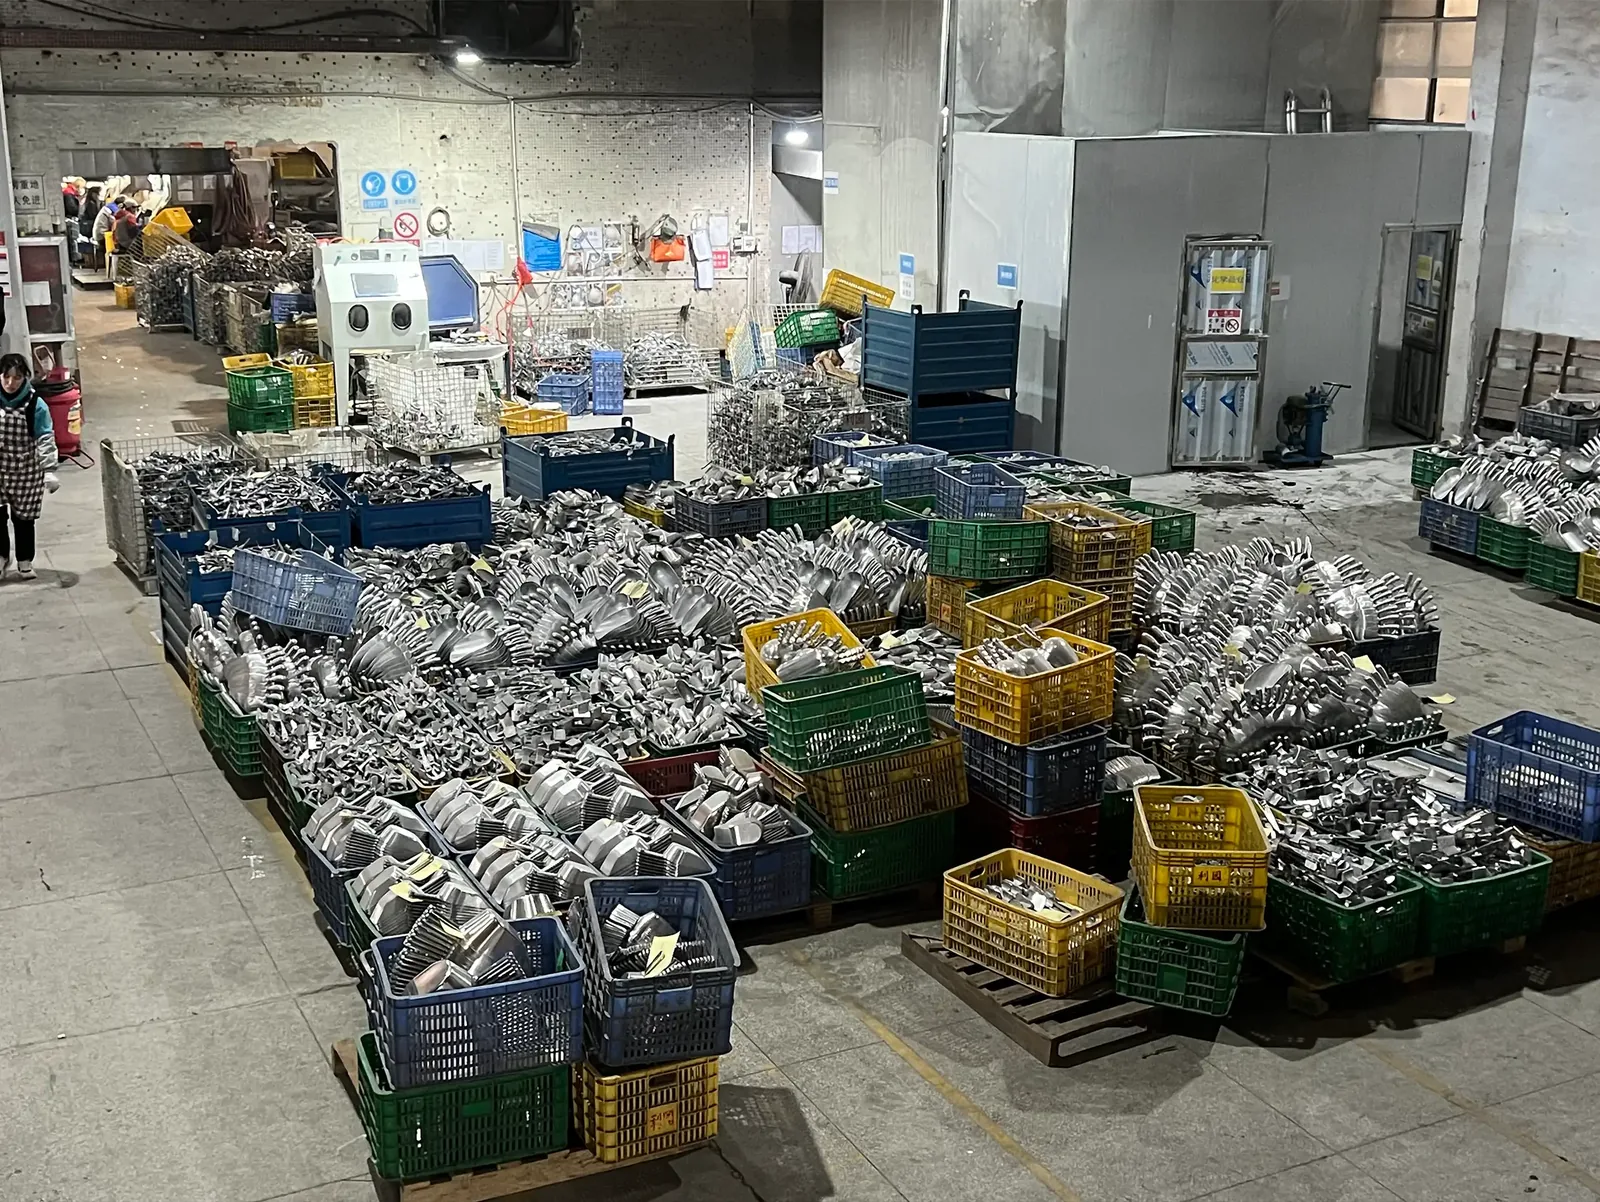
1 · Melting & dosing
Food-grade aluminum ingot held at 640–700 °C; each shot dosed to gram precision — over-dosing makes flash, under-dosing makes cold shuts.
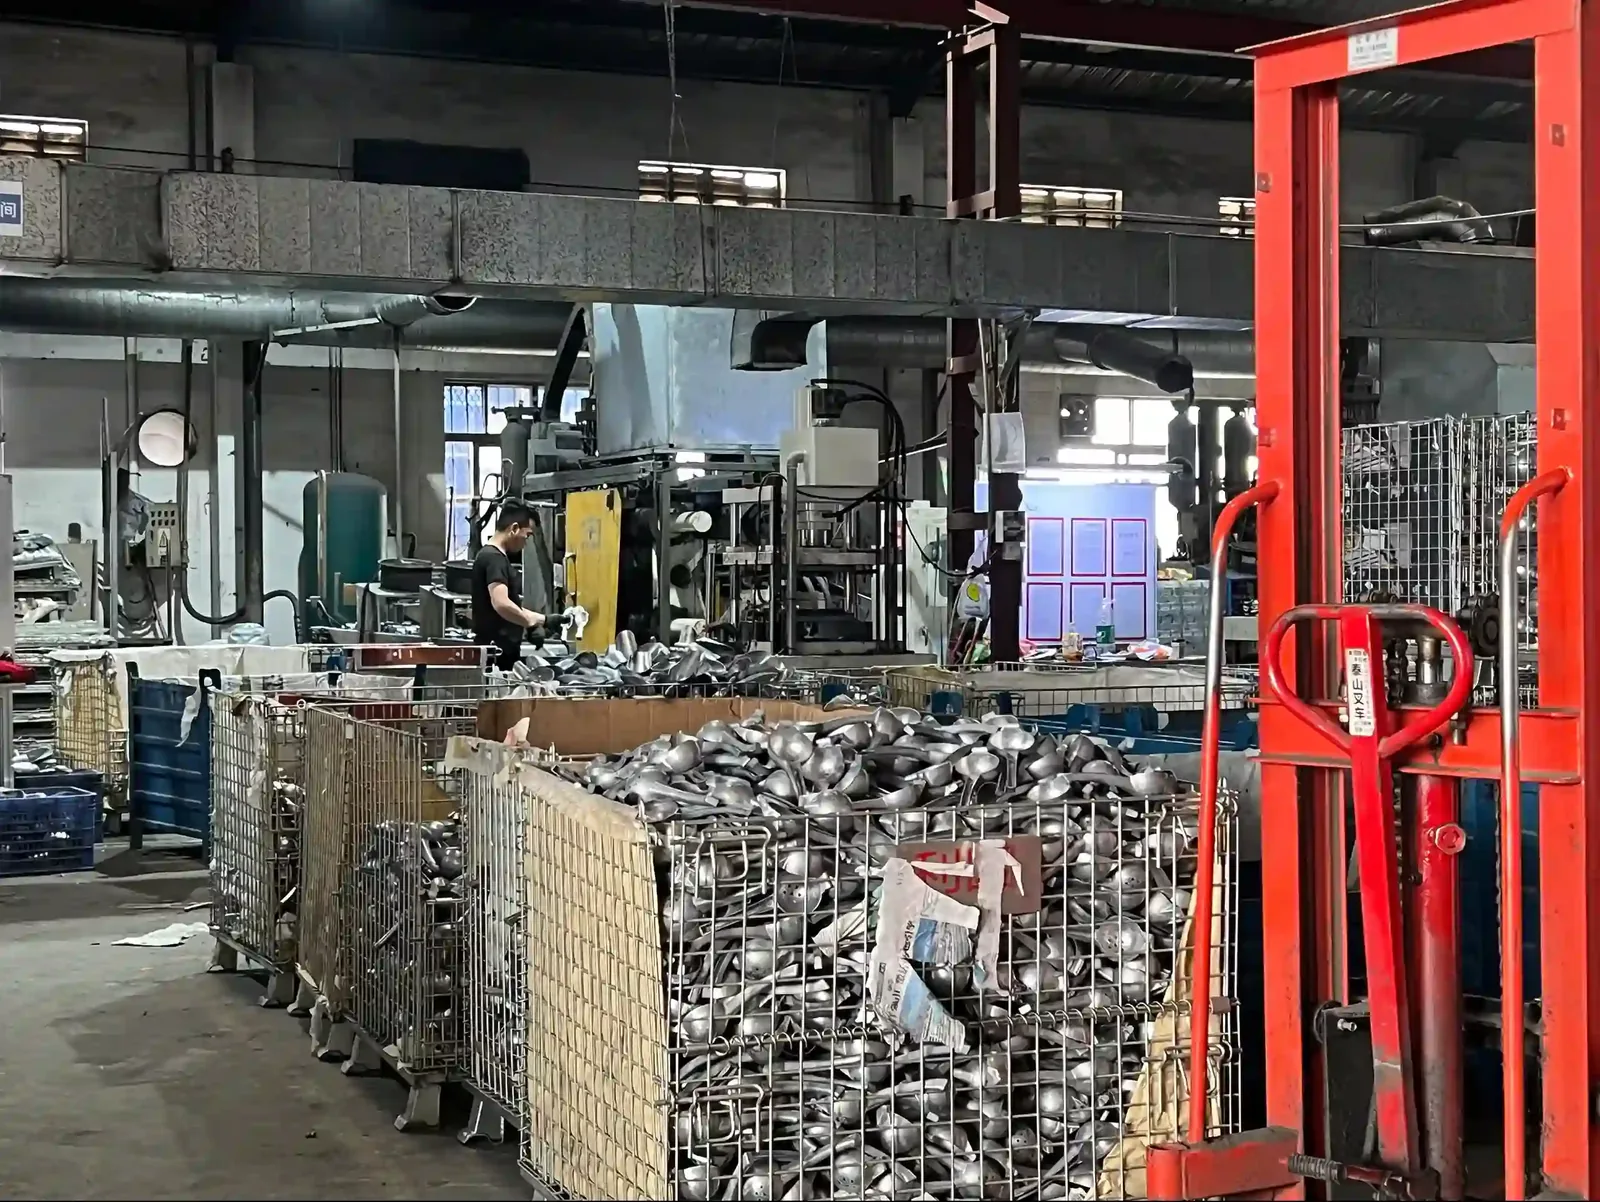
2 · Die casting
One-piece castings on our own presses: bowl, neck and handle formed in a single 40–60 second cycle. No welds, no seam failures.
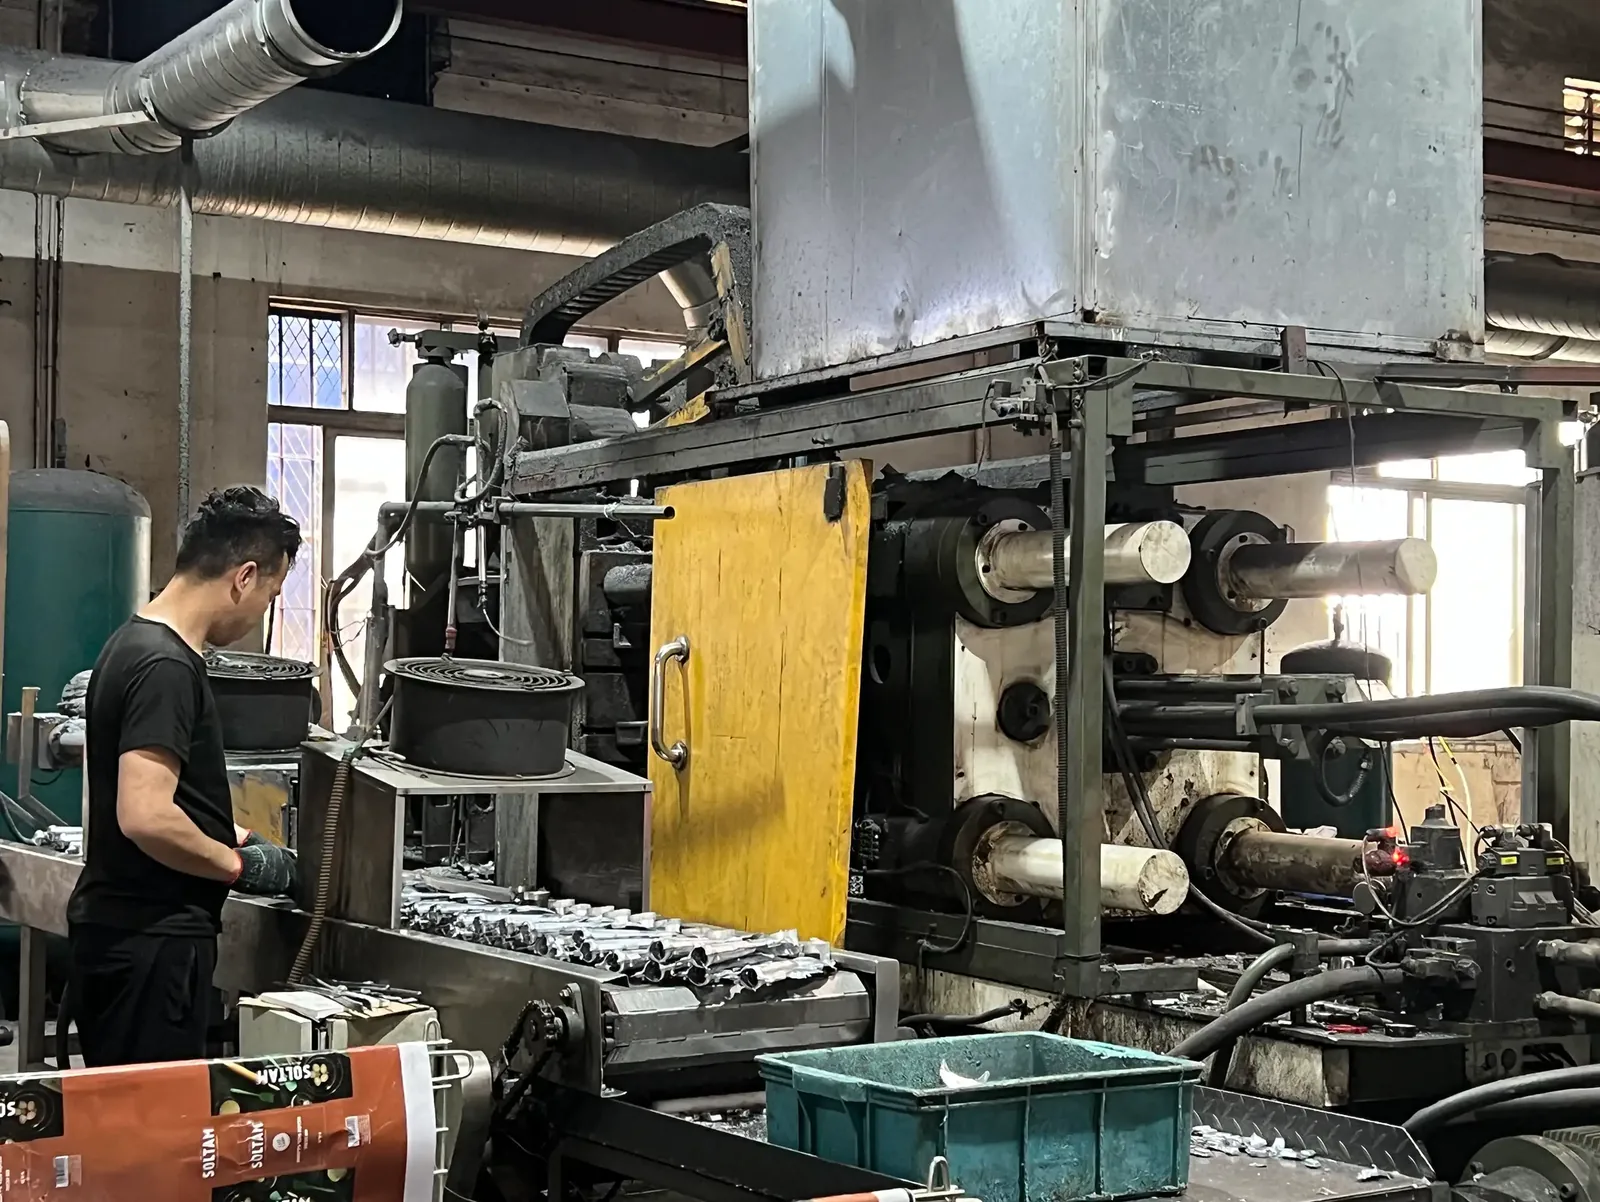
3 · Trimming & deburring
Gates and overflows trimmed while warm; edges deburred and inspected 100% visually at the trim station.
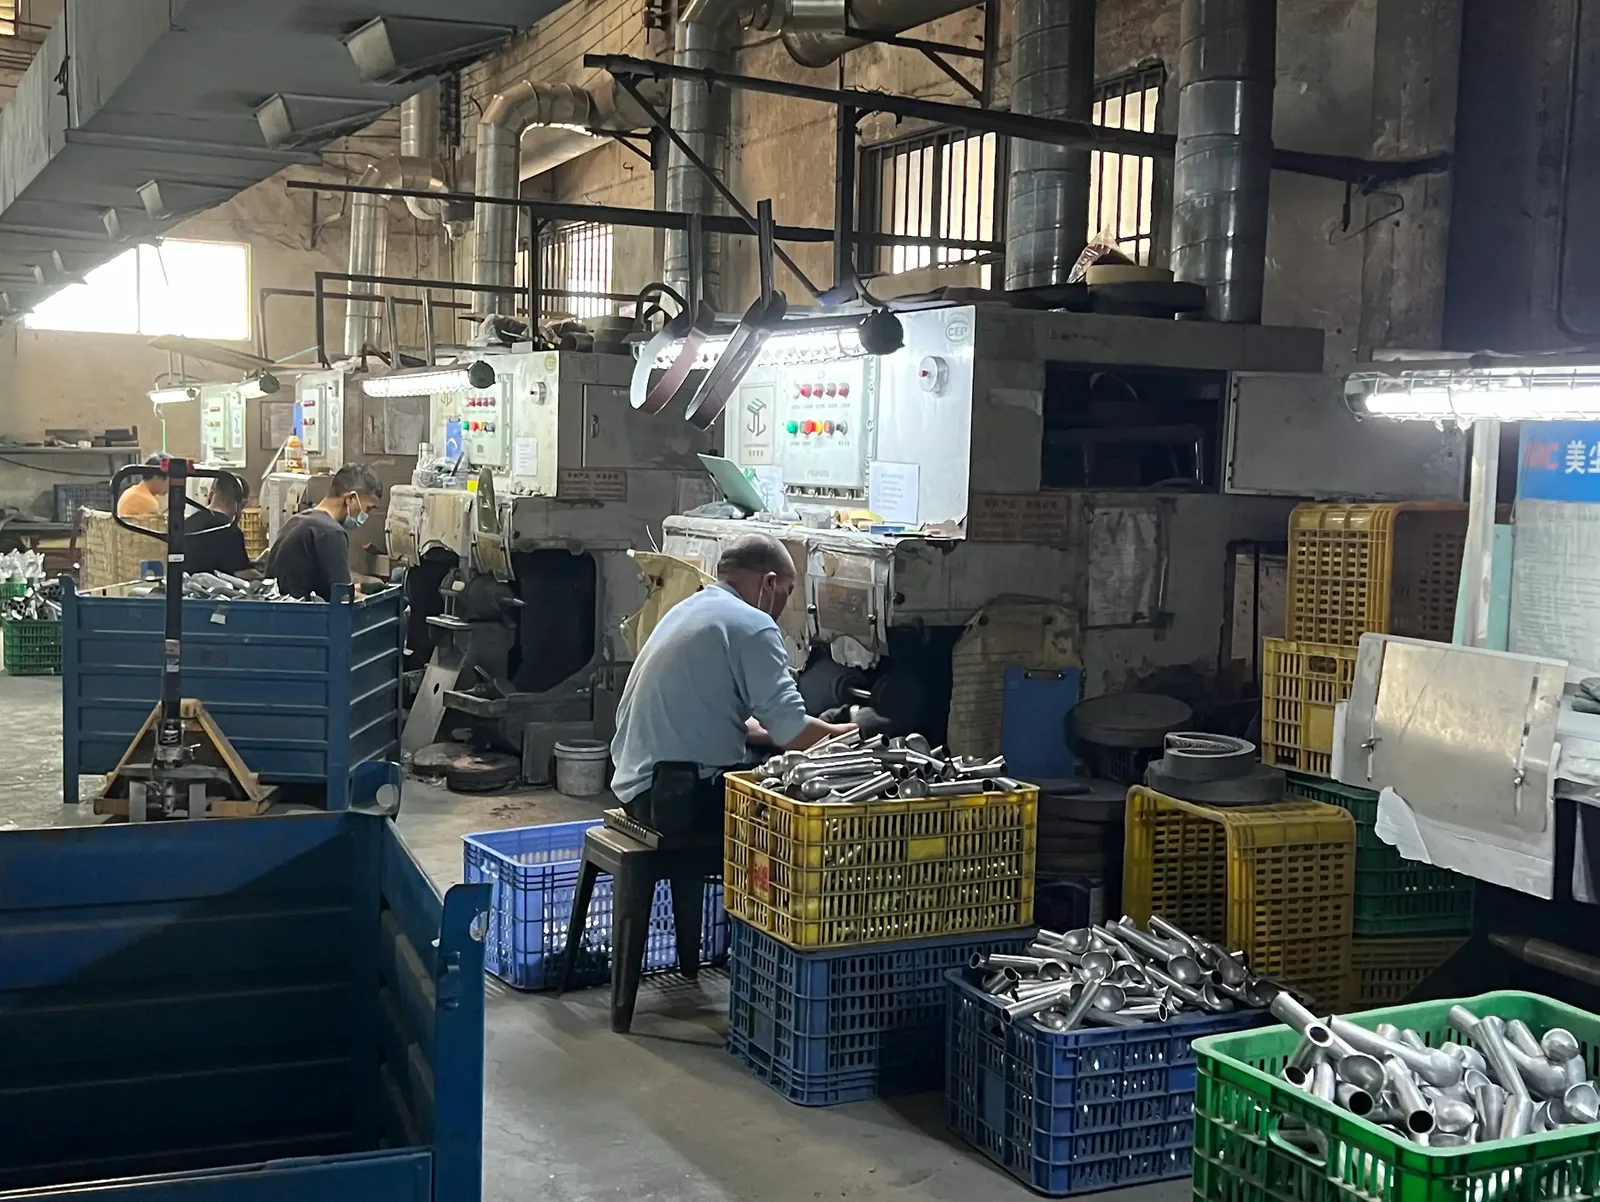
4 · Polishing & finishing
Tumble and hand polishing to satin or mirror; plated and PVD finishes for zinc components.
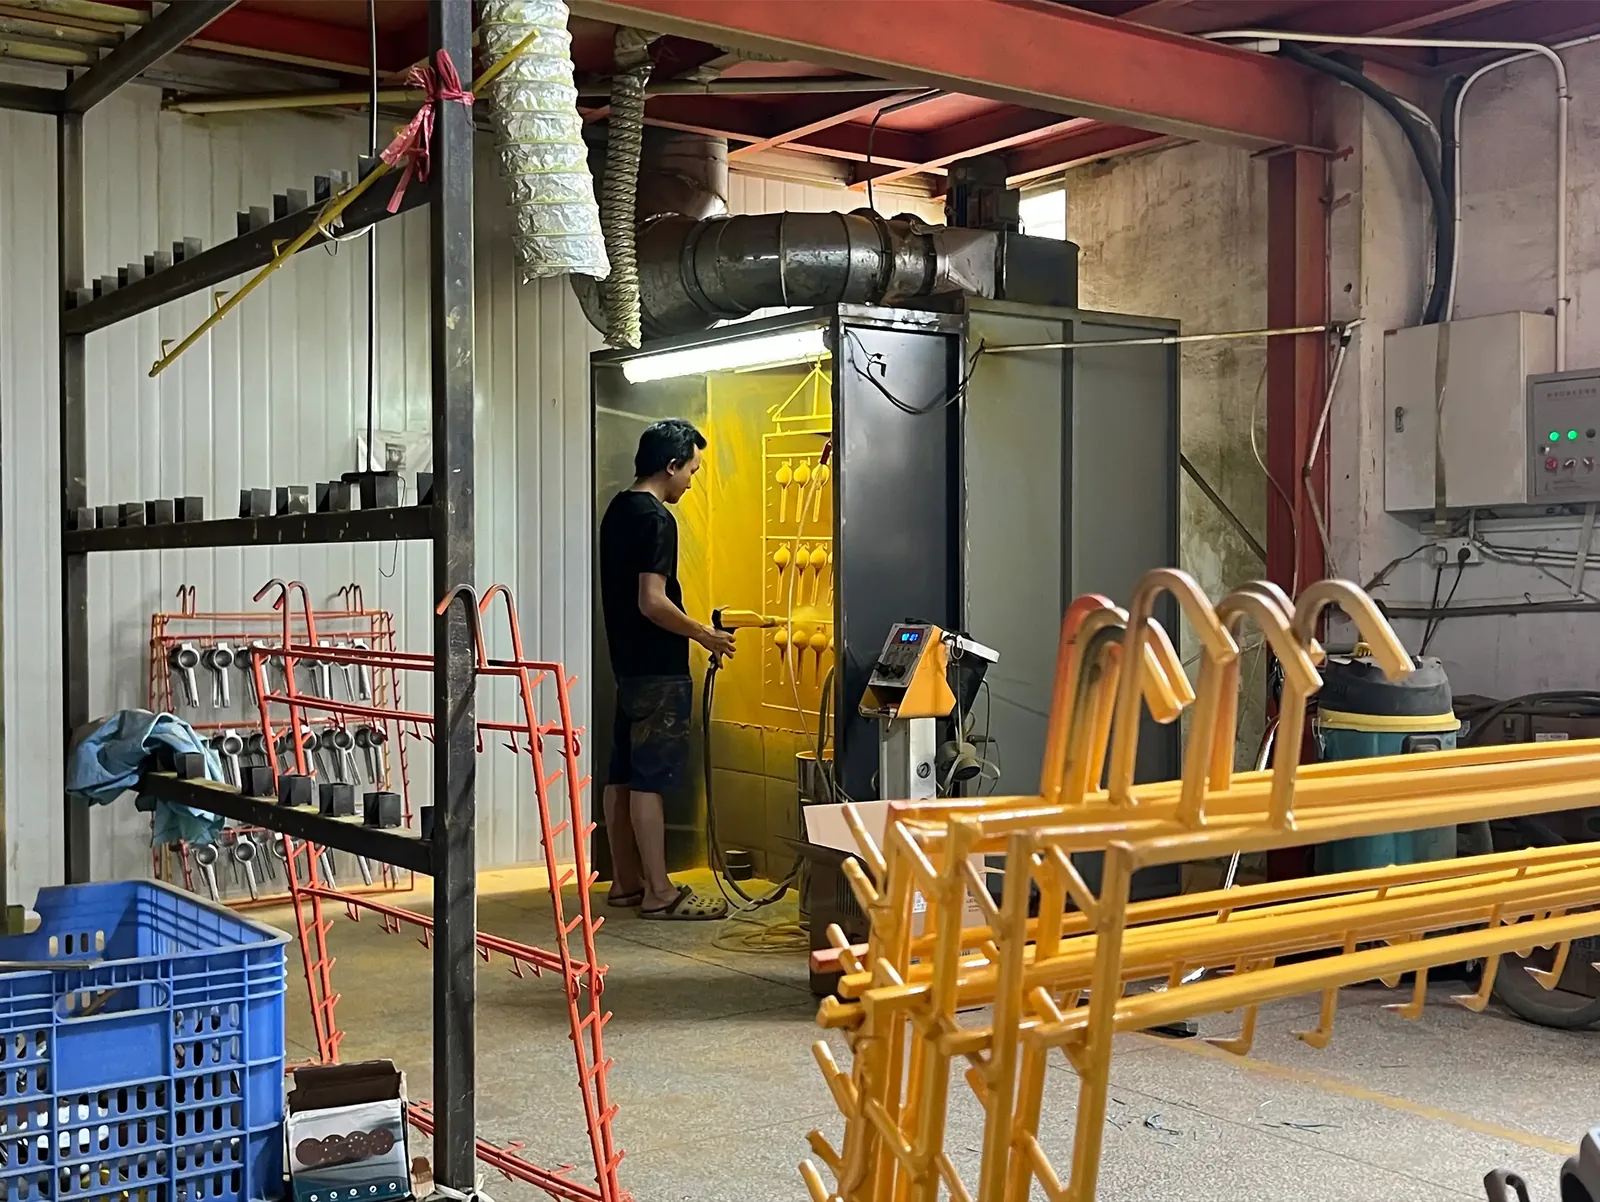
5 · Coating
Pantone-matched powder and liquid coatings, baked and adhesion-tested. FDA/LFGB per formulation.
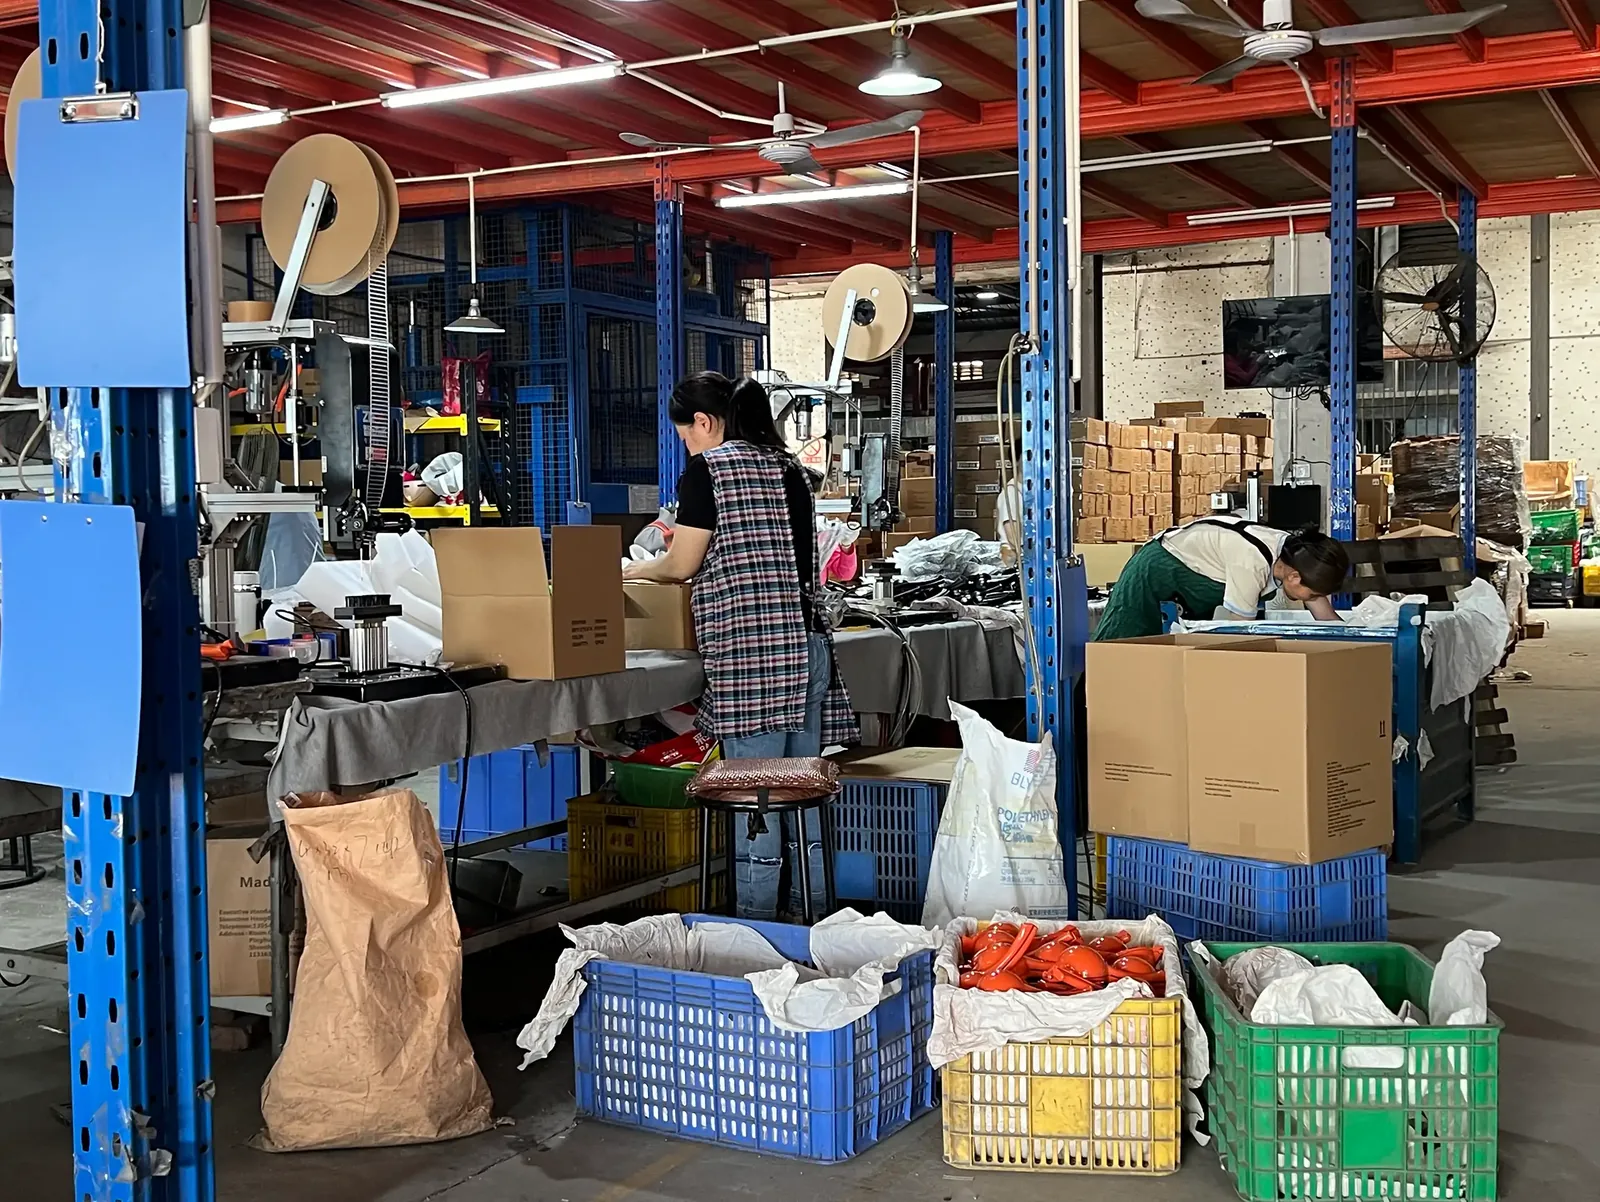
6 · QC & packing
AQL 2.5 final inspection, coating cross-hatch tests, handle torque checks — then retail or export packing.
Capacity & equipment
| Factory area | 3,400 m² total facility · 2,885 m² covered plant area per SGS report QIP-ASI251804 |
|---|---|
| Die-casting presses | Aluminum & zinc alloy presses, 88–268 t, in-house |
| Monthly output | 300,000+ pieces · 200,000+ pieces exported monthly |
| Warehousing | Turnover 40% faster than conventional; order dispatch within 7 days for stocked programs |
| Urgent orders | Priority scheduling line for urgent commercial programs |
| QC standard | ISO 9001:2015 · incoming certs · in-process checks · AQL 2.5 final |
What this means for buyers
- Cast-in-house = full control over porosity and finish quality
- Stocked fast-movers dispatch within 7 days
- New tooling 25–30 days, T1 samples 7–10 days after
- Factory tours and live video audits welcome